

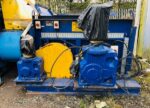
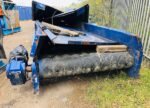


SOLD – Used BHS BB90R Bag Splitter
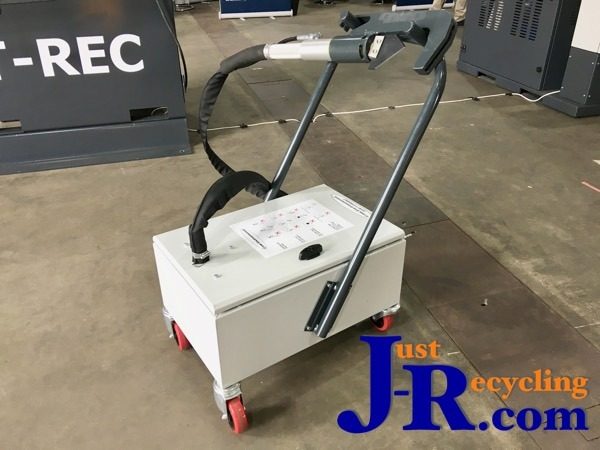
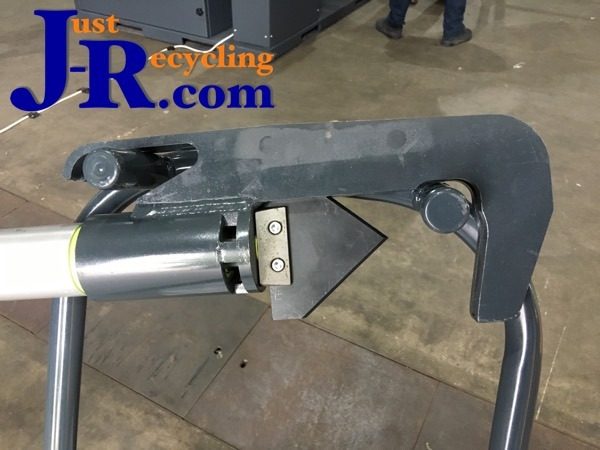
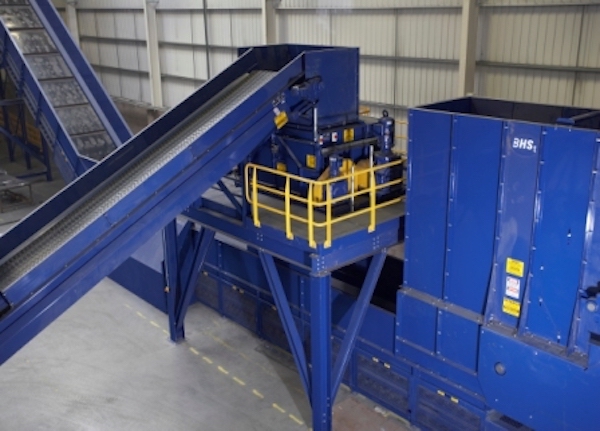
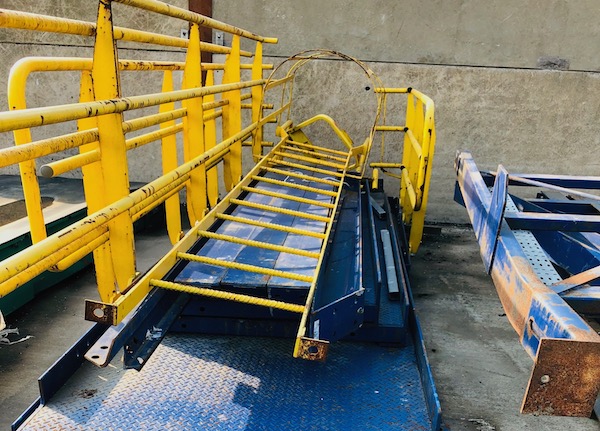
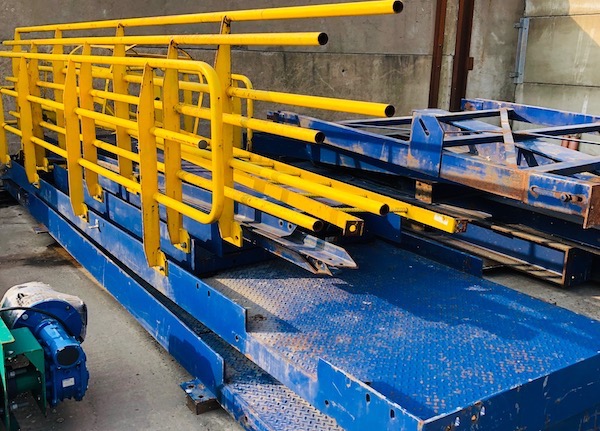
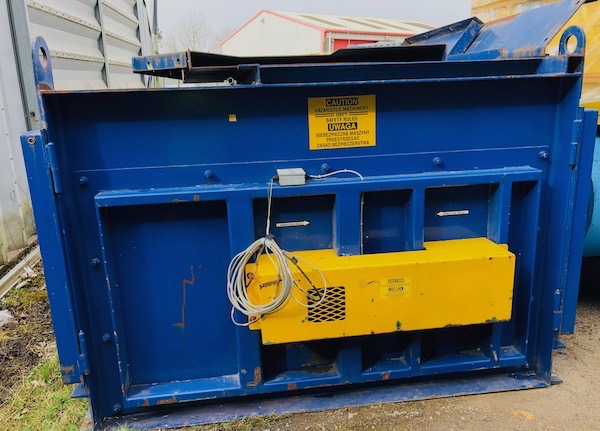
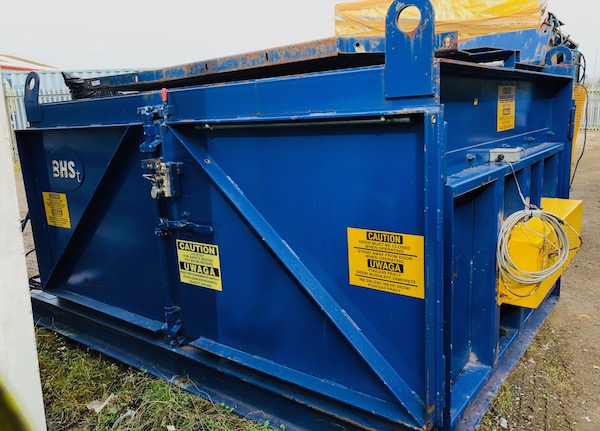
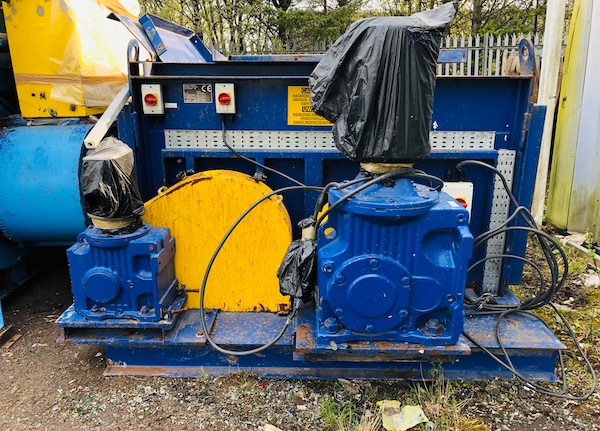
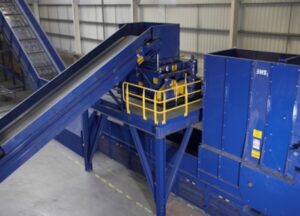
Sold The used BHS BB90R bag splitter is in full working condition is dismantled and ready to load to transport and is available immediately ex site UK.
SOLD Used BHS BB90R Bag Splitter
Item No: 14978
SOLD
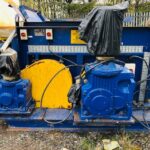
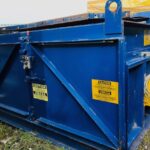
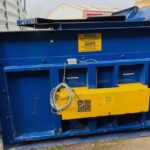
The used BHS BB90R bag splitter is in full working condition is dismantled and ready to load to transport and is available immediately ex site UK.
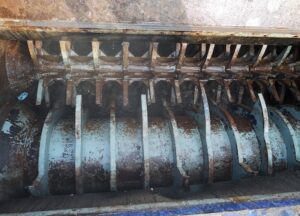
Removing the need for labour intensive manual bag opening the BB90R removes outer bags efficiently and fast.
Delivered new in 2009 from the market leading BHS stable the bag splitter or bag breaker comes as a stand alone unit or can be easily incorporated in to any existing recycling line.
Black bin bags, bagged clinical waste, bagged UBC’s and bagged plastic can all be processed to good effect in the used BHS BB90R bag splitter.
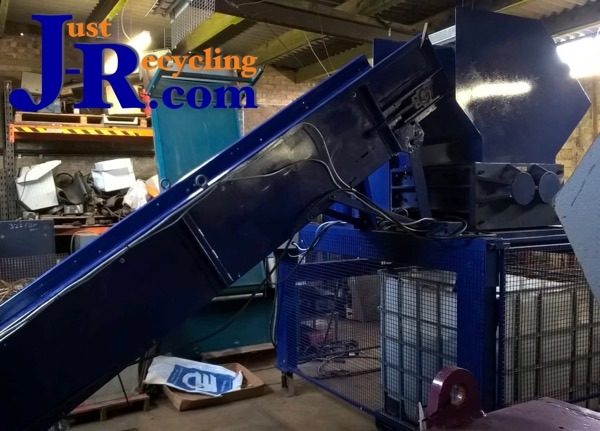
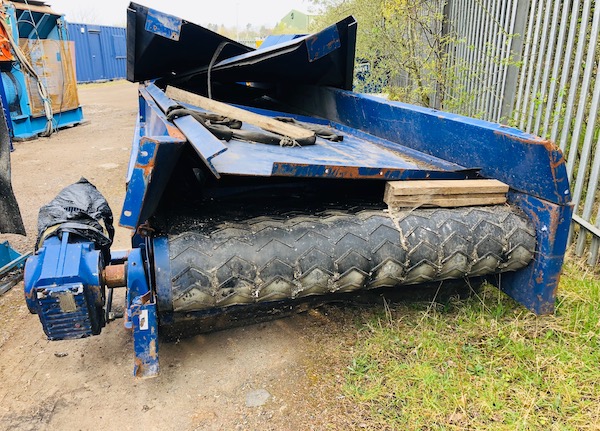
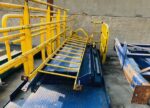
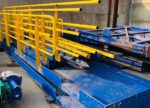
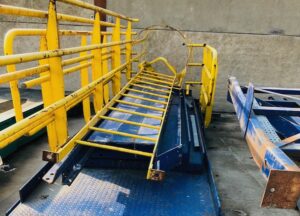
The splitter head comes with a steel support frame with access platform and stairs, an in feed conveyor and electrical control panel.
In good working order when removed from service the used BHS BB90R bag splitter is available immediately and good to go –
Price of the Used Bag Splitter:
£ SOLD + VAT
Ex site UK
Dismantled ready to load to transport
For further information or to make an appointment to view the used BHS machine for sale please email us or ENQUIRE NOW!
Need more information? Not quite what you are looking for? We can help. We have access to a huge range of new and used recycling machinery and recycling equipment at Just-Recycling, as well as recycling businesses currently for sale. Click Enquire Now, detailing your enquiry and one of the Just-Recycling team will contact you very shortly. We look forward to helping you.
Benefits of Owning a Bag Splitter –
- Higher processing capacity than manual sorters
- Low maintenance and operational costs
- Easy to retrofit into existing facility
- Does not damage bagged contents
- Clean-out doors on two sides for easy access and maintenance
- Heavy-duty construction for decreased downtime and long operating life

| Dimensions | 100 × 70 × 170 cm |
|---|
BHS (Bulk Handling Solutions)
Founded in 1976 and headquartered in Eugene, Oregon, BHS designs, manufactures and installs processing systems tailored to extract recyclables from the waste stream.
BHS is building the largest, most rugged and highest performing MRFs in the world. As a result, our customers are leading the industry with the highest throughput, recovery, and purity rates achieved anywhere. Simply put, our customers realize higher profits than their peers.
This early experience gave BHS insight into processing various types of material streams, knowledge that would prove invaluable as we set our sights on a new and emerging market – extracting recyclables from waste streams.
In 2013, BHS announced our European Headquarters, BHS Europe, based in Amsterdam, The Netherlands. BHS Europe manages sales, product delivery and customer service in Europe for the full range of BHS products and systems from BHS, NRT and Nihot.